
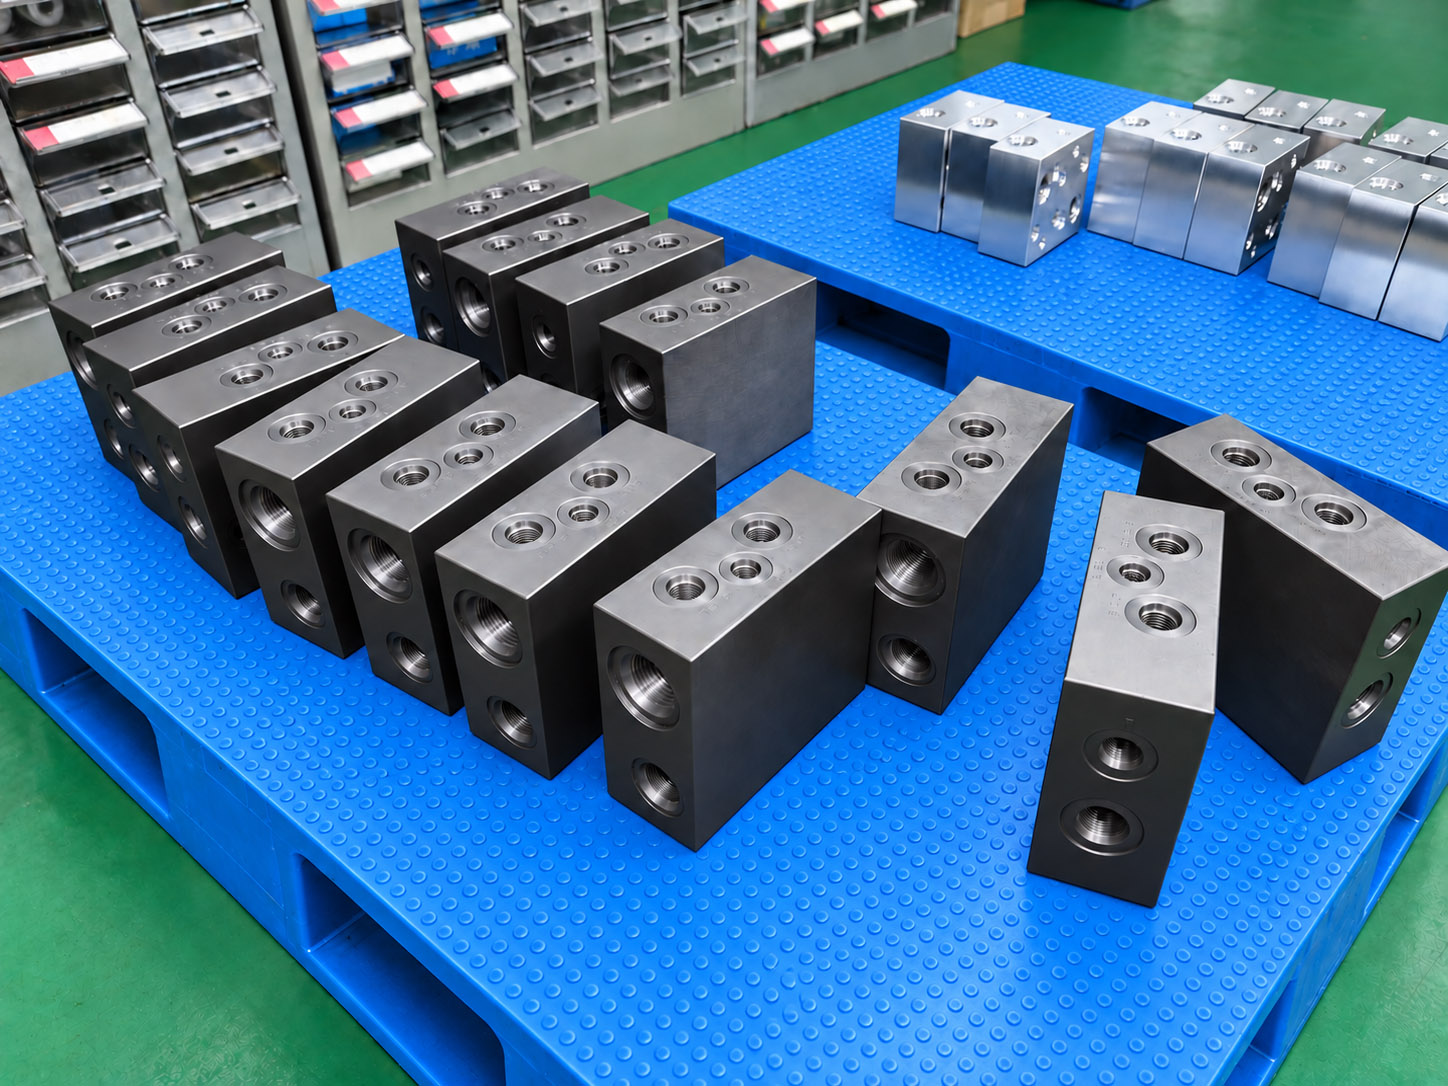
Define what the manifold must be like after treatment
A valve cavity that passes inspection before coating may no longer meet its final size afterward. A corrosion-resistant outer face may coexist with an inadequately protected internal passage. The finish therefore belongs in the manufacturing plan from the start, alongside the material, geometry and acceptance requirements.
Specify the finish completely
Identify the process, applicable specification and revision, coating requirements, final surface condition and any color or appearance reference. A note such as “black” or “anti-rust” leaves important decisions unresolved.
Identify where requirements apply
Mark treated and untreated areas, internal passages requiring protection, permitted contact locations and critical sealing or mating features. Resolve unclear boundaries with the design owner before release.
Define the acceptance stage
Clarify which drawing dimensions and surface requirements apply after treatment. Agree inspection locations, records, sample scope and the condition required for storage, shipment or assembly.
Surface treatment is coordinated with external processing suppliers as part of the manifold order. The scope and evidence required are agreed for the project; a finish name alone does not establish performance.
Protect the feature, not just the visible surface
Masking is a feature-specific instruction, not a default rule to leave every bore untreated. A surface may need both dimensional control and corrosion protection. Resolve that combination before choosing the machining allowance and treatment route.
| Feature | Risk to address | Control to agree |
|---|---|---|
| Valve cavities and sealing bores | Added or converted surface layers can affect diameters, transitions and the final sealing surface. | Define final dimensions and roughness, any permitted machining allowance, and the areas to coat or mask. Check the specified features in their accepted condition. |
| Threads and hydraulic ports | Treatment can affect thread fit and the relationship between the thread and its sealing feature. | Specify the final thread requirement and gauging stage. Review masking and coating allowance together with the port sealing surface. |
| Mounting faces and O-ring grooves | Surface preparation or treatment can change the condition of mating faces and groove features. | Keep final flatness, dimensions and surface requirements explicit. Define any protected areas and permissible contact marks. |
| Deep passages and blind regions | Access, drainage and process distribution can differ substantially from an exposed face. | Identify the coverage requirement and how it can be verified; plan rinsing, drying and subsequent corrosion protection. |
| Rework or machining after treatment | Removing a layer can expose base material or change a previously accepted feature. | Review rework with the applicable specification and design owner. Agree any repeat treatment and the checks required before release. |
Masking boundaries, coating allowances and any later finishing operation must be consistent with the approved drawing. We do not use one universal allowance for every finish or change a cavity dimension without authorization.
Review valve cavities and port interfacesSeparate exterior corrosion protection from internal coverage
For a steel manifold, protecting internal passages during storage and transport can matter as much as protecting the outside in service. Rust inside a passage can become a contamination source. Discuss the internal and external requirements separately, then assess a suitable treatment route.
Zinc and zinc-nickel plating
These are options for exterior corrosion protection. As electroplated finishes, coverage inside deep or recessed passages can be limited by current distribution and geometry. A satisfactory external coating does not prove the same layer is present throughout the block.
Electroless nickel
Chemical deposition avoids the current-distribution constraint of electroplating and can provide more even coverage on complex shapes. Internal coverage still depends on access, preparation and solution exchange. Define the required thickness, locations and acceptance evidence for the actual passage arrangement.
Black oxide (blackening)
Specify the blackening process and any supplementary protective oil or seal. Relate the required protection to storage and use, and verify the agreed surface and fit requirements. A dark appearance alone does not establish corrosion performance.
Phosphating
Agree the phosphate system, preparation, treated areas and any supplementary oil or sealer. Control process residues, rinsing and drying, and preserve the required valve-cavity, thread and sealing-surface condition.
An electroless-nickel layer followed by an external zinc finish is an optional route in Zhongwei’s project experience. It can be considered when internal protection and external corrosion requirements need different responses. It is not a standard treatment for every steel manifold; the sequence, layer requirements, supplier suitability and final dimensions need project approval.
No coating name establishes a universal salt-spray duration, outdoor life or suitability for every fluid. Any corrosion test must have an agreed method, specimen, acceptance criterion and reporting scope. External results do not automatically establish performance inside a deep passage.
Technical background: Anoplate on electroless nickel coverage. This explains a process principle; it is not evidence of a Zhongwei batch result or a supplier relationship.
Surface-treatment selection guideConnect the treatment route to the material and its condition
High-strength steel: manage hydrogen risk
For materials such as C35E+QT and AISI 4140, grade alone is insufficient. Review actual strength or hardness, heat-treatment condition, surface preparation and the applicable customer specification with the processor. Establish any required embrittlement-relief treatment, sequence and records before processing. A generic “baked” note does not define a complete control plan.
Aluminum: control appearance expectations
For 2017, 2024 and 7075, Zhongwei’s experience includes working with anodizing suppliers to improve appearance consistency. Alloy, material condition and processing can still affect shade and surface appearance. We do not promise completely uniform color or freedom from visible material variation. Agree representative samples and acceptable variation for appearance-critical work.
Where a stainless steel drawing specifies passivation or another surface process, keep its method, applicable specification, acceptance and delivery condition explicit as well. Do not substitute a finish merely because another material used it successfully.
References: ASTM B850 overview of post-coating hydrogen-embrittlement risk reduction and Aluminum Anodizers Council guidance on alloy and appearance. The applicable project specification governs; these references do not imply blanket certification.
Aluminum grades and anodizing considerations Stainless steel material requirementsKeep the weld-intended cylinder-end route distinct
For our Q355B and GB 45 valve-integrated cylinder ends and cylinder-head valve blocks intended for welding, the delivery route is machining followed by immersion in a no-clean rust-preventive oil and packing in a sealed, dust-protective PE bag. These components do not require plating, black oxide or phosphating for this supply route.
The no-clean rust-preventive oil used by Zhongwei allows welding without a separate cleaning or degreasing step to remove the protective oil. Here, no-clean refers to the subsequent welding operation. Confirm the preservation route against the customer’s welding procedure; this statement does not apply to other protective oils or remove other weld-preparation requirements.
Zhongwei uses approximately 3–6 months as an experience-based reference for this preservation route, subject to packaging and storage conditions. Dry storage helps maintain protection; moisture exposure, handling and damage to the bag or oil film can change the outcome. Agree the storage and transport requirements for the order rather than treating this reference as an unconditional rust-free period.
Customer feedback reported to Zhongwei describes parts protected with this oil and sealed in dust-protective PE bags that showed no rust after approximately one month of sea transport followed by more than one month in a warehouse. This is delivery experience for those conditions, not a controlled corrosion test or a guarantee for every shipment.
The production route identifies the agreed preservation, application and packaging requirements. Do not send these parts for black oxide, phosphating or plating by default, or replace the specified protective oil without reviewing the downstream welding requirement.
Cylinder-end valve blocks and material referencesKeep the processing supplier on the same revision
The handover should describe the part to be returned, including its protected features and required evidence. Zhongwei connects these instructions with machining and final inspection so the processor is not left to infer functional requirements from the outside of the block.
Before dispatch
Confirm material and condition, drawing revision, quantities, finish specification, masking map and agreed acceptance requirements. Clarify the current part condition and any handling restrictions.
Before processing
Resolve questions about internal coverage, rack or contact locations, appearance samples, inspection access and required records. Changes to the finish, masking or sequence need approval against the project requirements.
On return
Match the returned parts and processing records to the order and batch. Check the agreed features and condition before release. A mismatch or proposed rework needs disposition before the parts continue through the delivery route.
Check the finished condition, then preserve it

Geometry and surface condition
Verify the drawing requirements at the agreed stage, including applicable diameters, thread-gauge checks, mating features and sealing-surface roughness. The bore-measurement photograph at the top of this page illustrates dimensional inspection; it does not establish coating thickness or a post-treatment result for that part.
Finish evidence
Review the specified appearance, protected areas and processing records. Agree where coating measurements or other tests are required, who performs them and which parts or samples they represent. A visual check cannot establish hidden coating thickness, adhesion or corrosion-test performance.
Plan cleaning, rinsing or drying as appropriate to the finish and processing route. Address trapped residues, handling and any compatible temporary corrosion protection before packaging. Do not apply a later cleaning or rework method that compromises the specified layer.
Routine acceptance remains focused on material and drawing conformity. Pressure and functional testing are not routine checks for the machined block. Formal component-cleanliness testing, when required, is agreed separately from coating and dimensional inspection.
Inspection methods and their limits Cleaning, handling and packagingQuestions about finishing a hydraulic manifold
Can you coordinate black oxide and phosphating for steel blocks?
Yes, according to the agreed material, finish specification and processing scope. Define supplementary protection, functional surfaces and final acceptance. Weld-intended Q355B and GB 45 cylinder ends use their separate machined-and-oil-preserved route.
Should every valve cavity be masked before coating?
No. The decision depends on final size, sealing-surface requirements and whether the feature also needs protection. Define coated and uncoated areas, boundaries and final acceptance before choosing the machining allowance.
Does a coated outside mean the deep passages are protected?
No. Internal coverage depends on the process and the passage geometry. State which internal areas need protection and agree suitable evidence; an external appearance or thickness check alone does not establish hidden coverage.
Is electroless nickel plus zinc your default finish for steel blocks?
No. It is a project-specific option for combining internal and external protection needs. Confirm the layer sequence, requirements, material suitability, final dimensions and acceptance before using it.
Can threads simply be re-tapped after plating if they feel tight?
Re-tapping can remove the specified layer and change the accepted condition. Investigate the dimensional issue against the drawing and treatment specification, then agree an authorized rework route and any repeat inspection.
Can you guarantee identical black anodizing on every aluminum grade?
No. Different alloys and material conditions can respond differently. For appearance-critical parts, review representative samples and agree the acceptable range, viewing conditions and relevant surfaces.
Does every order include a salt-spray or coating test report?
No. The required test, method, sample or batch scope and report must be agreed for the order. A supplier process record and a part-specific test report provide different evidence.
What should we provide with the surface-treatment requirement?
Send the current part drawing, exact material and condition, finish specification, coated and masked areas, final dimensional requirements, appearance reference, exposure conditions and required records. Identify any incomplete requirements for review.
Send the part drawing together with the finish specification
Mark the critical cavities, threads, sealing faces and internal passages. Include the material condition, finish and masking notes, final tolerances, corrosion or cleanliness criteria, quantities and required reports. If the finish is still being selected, explain the environment and the main concern so the manufacturing implications can be reviewed.
Complete manifold drawings are preferred. Send DWG, DXF, PDF or JPG drawings and STEP, X_T, IGS or SLDPRT models by email or WhatsApp. A schematic can start the discussion; the treatment route needs an agreed part definition before release.
Prepare the project enquiry